Case Study: Handheld Emission Detection Device Prototyping & Development Case study: Handheld emission detection device prototyping and development. Multi-gas sensing with NDIR, electrochemical, and laser scattering sensors, STM32H7 firmware, sample conditioning, and cloud connectivity for field emissions monitoring.

Prototyping and Development of a Handheld Emission Detection Device

Adequate Infosoft has developed all stages of engineering services for the handheld emission detection project.

Our specialists were responsible for many components of product design and prototyping, including hardware architecture, various sensors integration, embedded firmware, thermal and airflow management, wireless communication, and prototype development.

We focused on developing compact, durable, and energy-efficient equipment that will measure multiple emission parameters.

Moreover, the project involved data transfer and cloud capabilities to ensure proper monitoring and analysis of the readings.

Through iterative prototyping and testing, Adequate Infosoft helped transform the concept into a functional field-ready device designed for reliable emission measurement in demanding environments.

1. Executive Summary

Project Chimera focused on developing a portable emission detection device capable of capturing real-time data from sources such as motorcycles and industrial exhausts.

The objective was to supply environmental and tax agencies with a dependable device for consistent and dependable emissions monitoring in the field.

The development took on significant engineering issues such as multi-mode sensors, management of heat and air, and most importantly a means of operating wireless in an energy-efficient manner and in a secure manner with the aid of the cloud.

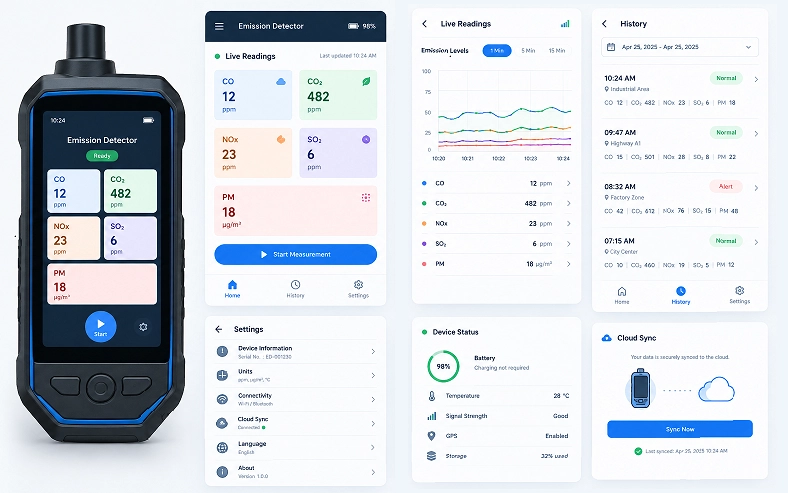
Designed for operation in demanding environments, the prototype integrates simultaneous measurement of CO, CO&sub2;, NOx, SO&sub2;, and particulate matter (PM). Weighing approximately 1.2 kg, the prototype demonstrated reliable field measurements with laboratory-level accuracy.

Prototyping and Development of a Handheld Emission Detection

2. Project Vision and Core Challenges

The main aim was to find a solution to the problems related to the utilization of expensive, delicate and bulky laboratory gas analyzers used for spot emission testing.

In order to successfully accomplish the goal, a small rugged emission device was to be created and worn in a safety belt close to exhaust systems and providing an accurate emission profile in a few seconds.

Portability and accuracy presented numerous engineering challenges such as sensor integration, supervision of thermal conditions, airflow supervision, stability of measurements, energy efficiency, and reliability under difficult field conditions.

Diversity in sensors and miniaturization:

Combining technology capable of detecting gases with different chemical characteristics (reducing and oxidizing) into a single handheld enclosure.

Robustness:

The device has to work in temperature conditions ranging from -10°C to 50°C, be able to withstand falling onto concrete, resist dust and moisture (inscription of IP65 class), and be resistant to vibration from machines nearby.

Sample Conditioning:

The exhaust output of a diesel generator can be as much as 300°C and filled with water and soot. Such a harsh sample has to undergo conditioning in order to transform it into suitable material for sensitive and stable sensors, without losing the necessary analytes.

Power Management:

The equipment built to operate for a complete 8-hour shift on a single battery charge, making it possible to combine the high energy consumption of the pumps and heated sensors with the requirements for mobility.

Data Integrity and Connectivity:

In places where network coverage is unreliable, the device has to keep data locally and safely, before syncing to the cloud dashboard (including GPS coordinate and timestamps) when connectivity is recovered.

3. Hardware Architecture and Prototyping

Our approach was to build on a modular architecture, allowing us to iterate on individual subsystems (sensor block, pump system, mainboard) independently before integration.

3.1. Multi-Modal Sensor Selection

Selecting the right sensor technology was the foundation. A single technology cannot adequately detect all target gases. We opted for a hybrid approach:

Non-Dispersive Infrared (NDIR) Sensors:

These sensors are selected for the purpose of detecting CO2 and hydrocarbons (HC). We come up with a dual-channel NDIR module of Senseair (Sunrise Series).

The dual-channel technology provides the reference channel to allow the automatic compensation for light source aging and drift which is important for field stability for long term. The optical path of the sensors has been miniaturized by employing gold-plated reflective cells to provide the sensitivity in compact packages.

Electrochemical (EC) Sensors:

Selected for toxic gases: Carbon Monoxide (CO), Nitrogen Dioxide (NO2), and Sulfur Dioxide (SO2). We used 4-series sensors from Alphasense, specifically their "A4" and "B4" variants, which offer high sensitivity and low cross-sensitivity. Each sensor was mounted on a custom-designed potentiostat circuit.

This analog front-end (AFE) uses a transimpedance amplifier with a programmable gain and a low-pass filter to convert the nano-ampere-level current from the sensors into a clean, digitizable voltage. The key here was using a zero-bias configuration for NO2 and a biased configuration for CO and SO2 to optimize their redox reactions.

Laser Scattering for Particulate Matter (PM):

In order to measure PM2.5 and PM10, we utilized an optical particle counter. A laser diode is included in the sensing device (initial prototypes used the PMS7003 model from Plantower).

As particles pass through, the light is scattered, and the pulse amplitude is used to determine particle size.

Furthermore, we designed a custom inlet nozzle in such a way that there is no discrimination based on the inertia during the sampling process since the gas entering the device moves with the same speed as the flow through the exhaust.

3.2. Sample Handling and Conditioning System (The "Lung" and "Airway")

The sample handling system was the most mechanically complex part of the prototype.

Probe and Umbilical:

This apparatus utilizes a removable 1-meter stainless steel probe with an open-tipped end. We can connect this probe to the unit by means of a special cord made of high-temperature silicone which has a thermocouple (type k) for measuring exhaust temperature as well as a gas line.

The "Airway":

The unit contains a carefully designed path for gas. The main tube is made of PTFE (Teflon) to avoid getting problematic gases like NO2 and SO2 stuck to the tube, leading to measurement errors.

The "Lung" - Conditioning Block:

This is a custom-machined aluminum block containing:

A cyclone separator:

Gas enters tangentially, creating a vortex. Centrifugal force throws heavy soot and condensed water droplets to the walls, where they coalesce and are drained into a removable waste trap. This is a passive, no-maintenance primary filter.

A thermoelectric cooler (TEC):

The cooling process brings the gas temperature from about 300C down to 4C to guarantee the safety of EC sensors and NDIR light source. The prior working temperature greatly contributes to the moisture development, leading to the formation of a dry gas sample as a result of possible condensation.

Enormous engineering task is also related to stopping the whole "acid condensation" phenomenon. In case the gas is cooled too quickly, NO2 and SO2 gases get dissolved in the gas condensate and are transformed into nitric and sulfuric acids.

Such processes do not just harm the equipment but also result in incomplete detection of gases thus causing incorrect readings. Therefore, to avoid any problems, we use the permeation dryer stage right after the stage of initial cooling.

The sample passes through a Nafion tube, the tube's selective membrane allows water vapor to pass out to a dry purge gas, removing residual moisture without affecting the concentration of the target gases.

A micro-diaphragm pump:

A brushless DC pump is placed after the conditioning block to draw the sample through the system. Placing it downstream prevents the pump's internal components from contaminating the clean sample and keeps it protected from hot, dirty gas.

3.3. Enclosure and Ruggedization

We used a hybrid manufacturing method for this prototype. The chassis was machined out of a solid block of 6061 aluminum to ensure structural strength and electromagnetic interference (EMI) protection.

Following this, we applied a layer of thermoplastic polyurethane (TPU) on the aluminum chassis, which is 3mm thick.

The sensitive components (sensor block, main PCB) are mounted on a floating sub-chassis isolated from the outer shell via silicone dampers to absorb shock and vibration. All external connections (USB-C, probe port) use IP67-rated, bayonet-locking connectors.

4. Embedded Systems and Firmware

4.1. Main Processing Unit

The processor employed in the device is the STM32H7 series MCU by STMicroelectronics based on ARM Cortex-M7 architecture with a clock frequency of 480 MHz.

Such an MCU has been selected due to its high performance level required for real-time processing, as well as due to its multitude of peripherals (including ADCs, DACs, UARTs, SPI, I2C, etc.).

4.2. Signal Processing and Control

The firmware is written in C/C++ using FreeRTOS for real-time task scheduling. Key tasks include:

Sensor Data Collection:

A 16-bit ADC receives input from the conditioned signals of the gas sensor AFEs at a frequency of 10 Hz. The firmware makes use of a median filter to eliminate unwanted spikes in the signal and a moving average filter for smoothening purposes.

Cross-Sensitivity Compensation:

The raw readings from the EC sensors are influenced by other gases. For example, the SO2 sensor will respond somewhat to NO2. Our firmware applies a correction matrix, derived from laboratory calibration, to correct for these cross-sensitivities in real-time.

Environmental Compensation:

The NDIR and EC sensors are temperature-sensitive. Firmware reads the internal temperature and humidity of the sensor block and applies compensation algorithms based on the manufacturer's datasheets and our own lab testing.

Control Loops:

A PID (Proportional-Integral-Derivative) controller in the firmware manages the pump speed to maintain a constant, pre-set flow rate (e.g., 300 ml/min) through the system. Another PID loop controls the power to the TEC cooler to maintain the sample gas at the target 4°C.

4.3. Connectivity and Cloud Synchronization

The device features a tri-mode wireless module:

Bluetooth Low Energy (BLE):

Used for local configuration and diagnostics via a smartphone app.

Wi-Fi:

For high-speed data upload when in range of a trusted network (e.g., back at the office).

4G LTE Cat-M1:

For directly connecting through an LPWAN (low-power wide-area network), it is the basic means of transmitting data from the ground level.

The device operates using an MQTT protocol to send data to the cloud broker (AWS IoT Core). It is an efficient and simple protocol perfect for unstable networks.

The data packet includes a unique Device ID, a cryptographic signature for tamper-proofing, timestamp, GPS coordinates, a photo of the vehicle's license plate (taken by an integrated camera), and the processed emission readings.

If no connection is available, data is stored in a queue on a 64GB industrial-grade flash memory and uploaded automatically when connectivity resumes.

5. Power Management

The device operates via a removable 18650 lithium-ion battery that comes in a total capacity of 98 Wh. Meanwhile, the power supply system employs several buck and boost converters to deliver power in clean and efficient manner for the digital section (3.3V), analog section (5V) and high-power section (12V for pump/TEC).

The firmware uses aggressive power management, switching the NDIR sensor and TEC into low-power sleep modes when the device is idle and gating power to unused subsystems, achieving a continuous operational time of 10 hours.

6. Prototyping, Testing, and Validation

The prototyping process that we went through was very iterative. We initiated the process using a Level 1 (L1) "Franken-Device" made on a breadboard by utilizing readily available evaluation boards to demonstrate the working of the sensor fusion concept.

Then we moved to a Level 2 (L2) prototype where the integration of the components took place on our custom-designed PCBs and encased them within a 3D-printed housing for improving the mechanical configuration and initiating thermal testing.

Validation against reference gases in a controlled laboratory was critical. We used a gas calibration system (e.g., Environics 6100) to generate precise concentrations.

We calibrated each sensor and then tested the fully integrated L2 prototype against simulated exhaust mixtures. The results were promising: accuracy for CO and NO was within ±5% of the reference value, and the PM sensor correlated well with a reference photometer.

The final Level 3 (L3) Prototype was used for field trials. We subjected it to:

  • Drop tests: Repeated drops from 1.5m onto concrete.
  • Thermal cycling: Cycling between -10°C and +50°C in an environmental chamber.
  • Vibration testing: On a vibration table simulating a vehicle's dashboard.
  • Real-world testing: Attached to a diesel truck, a gasoline car, a 2-stroke generator, and a small industrial boiler.

The field trials were invaluable. They revealed a condensation issue in the probe line on humid days, which we fixed by adding a heated probe line. They also showed the need for a better user interface, leading to the inclusion of a high-brightness, glove-friendly, 4.3-inch touchscreen display.

7. Conclusion and Future Iterations

The outcomes of L3's final prototype successfully achieved the primary objectives set for the project and bring an affordable, mobile, and reliable emission detection system. The difficulty of simultaneous multi-gas measurement, sample treatment and power control has been solved thanks to various sensor choices, precise electro-mechanical construction, and stable firmware.

The next iteration (V2.0) will focus on:

Cost Reduction:

The NDIR sensor and the custom-machined conditioning block are the most expensive components. We will explore alternative suppliers and design for manufacture (DFM) to reduce unit cost.

Increasing Sensors:

Incorporating a PID for measuring VOCs, one of the main contributors to pollution from some industrial activities.

Technological Innovation:

Utilizing data to build models for predictive maintenance and instantaneous detection of emission deception tools.

Miniaturization:

Shrinking the overall form factor by moving to a custom System-on-Module (SoM) and a more integrated sensor manifold.

The EcoSentry prototype has proven that a high-fidelity, field-ready emission analysis tool is not only feasible but can be a powerful instrument in the global effort to monitor and reduce air pollution.

Abhinav Akula
DevOps Engineer and 3× Microsoft Azure Certified professional specializing in Azure cloud solutions, migration, deployment automation, and multi-cloud environments. He holds Microsoft certifications as an Azure Developer Associate and Azure Solutions Architect Expert, with expertise in building scalable, secure, and reliable cloud infrastructure.

What Our Clients Say About Us

Client satisfaction is our ultimate goal. Here are some kind words of our precious clients they have used to express their satisfaction with our service.

Leadership That Leads Worldwide

With a physical presence in over 15 countries and a global footprint spanning 25+ countries, we are ready to serve you anywhere. Location, language, or culture is never a barrier, because our global team can work with you in your language. Our strong international team ensures seamless collaboration across borders We have a strong tech team, highly recognized in their domains, with extensive technical expertise.